 | Hot-cast industrial polyurethanesMDI · TDI · PPDI · NDI POLYURÉTHANES INDUSTRIELS COULÉS À CHAUD — GUIDE DE SÉLECTION |
At Soremag, we hot-cast our polyurethane rollers and molded parts. The diisocyanate (MDI, TDI, PPDI, NDI) forms the rigid backbone — thermal resistance, load and fatigue — while the polyol (ester or ether) governs resistance to water, chemicals and solvents.
⬇ Download the PDF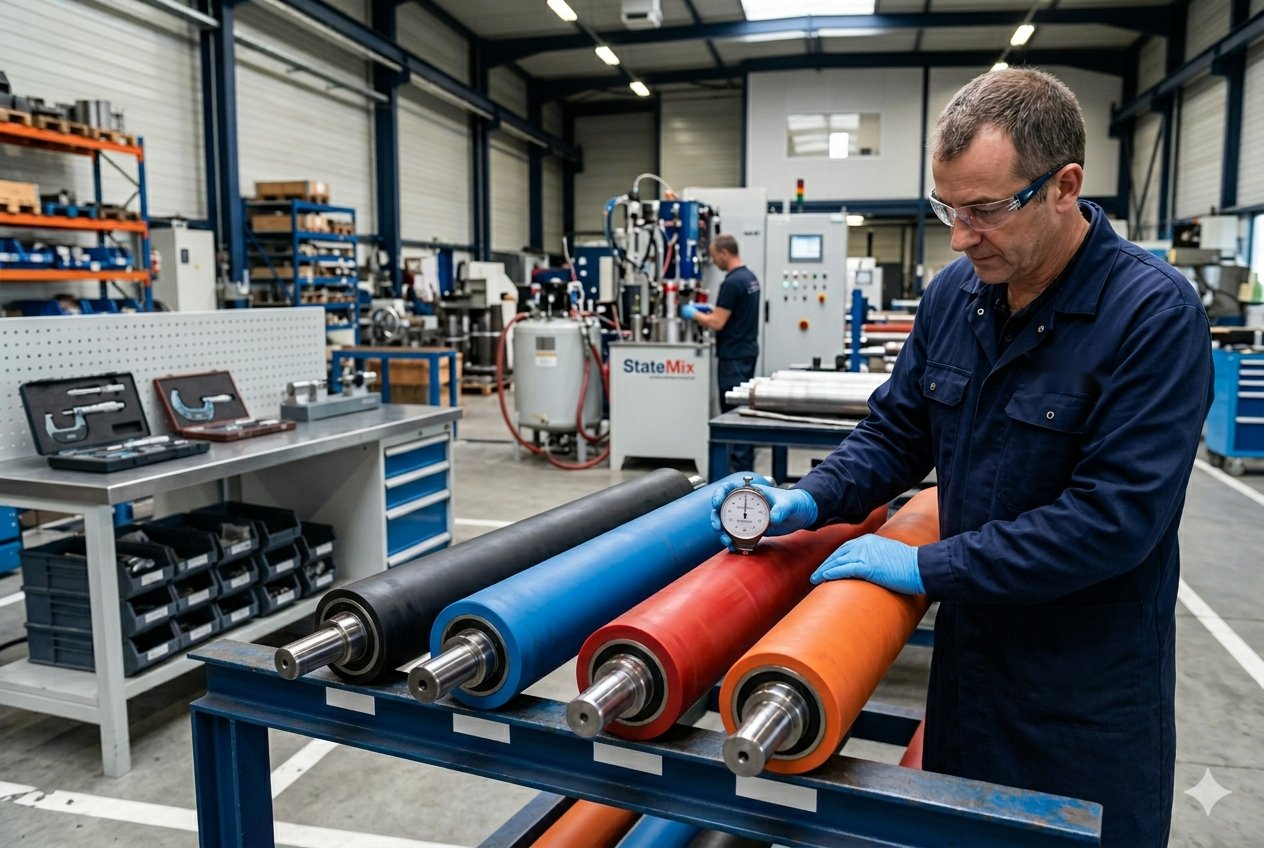
Soremag workshop — hot casting and hardness testing of polyurethane rollers and molded parts.
General data.
The values in this sheet are recognized material-level trends; actual performance depends on the formulation, hardness, curative and post-cure — several recipe developments can target different properties. Soremag formulates to spec.On a roller (covering)
- Abrasion:typically lasts 3 to 4× longer than rubber in abrasive environments — less downtime.
- Load:carries far heavier loads without crushing — heavy industry (metallurgy, mining).
- Non-marking:leaves no marks (unlike black rubbers) — paper, textile, finished goods.
- Cut / tear:resists better, and a nick does not propagate as it does on rubber.
- Chemistry:better resistance to oils, greases, ozone and some solvents.
On a molded part
- Hardness range:from very soft (Shore A) to plastic-hard (Shore D) while keeping elasticity.
- Metal adhesion:bonds to metal inserts far better than rubber — cored wheels, motor mounts.
- Reduced tooling:cast at low temperature and atmospheric pressure → cheaper molds (resin, aluminum).
- Machinability:hard parts can be machined (milling, turning) almost like metal for tight tolerances.
Polyester (ester)
Superior mechanical robustness: cut, tear, sliding abrasion, sealing against oils, fuels and aliphatic solvents. Good dry aging. Weak point: sensitivity to hot water (hydrolysis).
Polyether (ether)
Preferred in wet or washed environments: remarkable resistance to hydrolysis and microbial attack, higher rebound, low heat build-up, low-temperature flexibility. Pure mechanical strength and hydrocarbon resistance lower than ester.
Hot cast
The Soremag industrial standard
- Prepolymers and curatives heated (≈ 70–120 °C), mixed, then cured several hours in an oven.
- Extreme mechanics(abrasion, tear, impact) and superior dynamics: handles hysteresis where a cold-cast PU would melt.
- Massive load capacitywithout permanent set · very high hardness (up to Shore D) with impact resistance.
Cold cast
For context
- Two liquids (A + B) curing at room temperature — simple, economical, fast demolding.
- Ideal for prototyping, soft molds, static parts and electronic potting.
- But low dynamic durability: wears or degrades quickly in industrial settings.
The verdict —
for a conveyor roller or a part subject to friction, impact or heavy loads, hot casting is the way to go: it's our standard. Cold casting, while simpler, would wear out fast under dynamic stress. This hot-cast mastery is what sets Soremag apart.| MDI ester | MDI ether | TDI ester | TDI ether | PPDI | NDI | |
|---|---|---|---|---|---|---|
| Cold water (short contact) | G | VG | G | VG | VG | G–VG |
| Immersion / constant humidity | P–F | E | P–F | E | VG | F–G |
| Hydrolysis / hot water | P | VG | P | VG | VG | F–G |
| Steam | NR | P | NR | P | F–G | F |
| Oils & greases | VG | G | VG | G | VG | VG |
| Diesel & fuels | G–VG | F–G | G–VG | F–G | G–VG | G |
| Aliphatic solvents | G–VG | F–G | G–VG | F–G | G–VG | G |
| Aromatic solvents | P | P | P | P | F–P | F–P |
| Ketones, MEK, chlorinated solv. | NR | NR | NR | NR | P–NR | P–NR |
| Weak dilute acids | G | F–G | G | F–G | G | G |
| Strong acids | NR | NR | NR | NR | NR | NR |
| Ozone | G–VG | G–VG | G–VG | G–VG | G–VG | VG |
| Low temperature (flexibility) | F | VG | F | VG | G–VG | F–G |
| Continuous heat | G | G | G | G | VG | G–VG |
E Excellent
VG Very good
G Good
F Fair
P Poor
NR Not recommended
| MDI ester | MDI ether | TDI ester | TDI ether | PPDI | NDI | |
|---|---|---|---|---|---|---|
| Abrasion | VG | G–VG | VG | VG | E | E |
| Cut | VG | G | VG | G–VG | E | E |
| Tear | VG | G | VG | G–VG | E | E |
| Tensile strength | VG | G–VG | VG | G–VG | VG | E |
| Rebound / resilience | F–G | VG | F–G | VG | VG–E | E |
| Low hysteresis (heat build-up) | F | G–VG | F | G–VG | VG–E | E |
| Dynamic fatigue (flex) | F–G | VG | G | VG | E | E |
| Compression set | G | G–VG | G | G–VG | E | E |
| Load capacity | G–VG | G–VG | G–VG | G–VG | G–VG | E |
| Heat resistance (service) | G | G | G–VG | G–VG | E | VG |
| Dimensional stability | G | G | G | G | VG | VG–E |
| Castability | VG | VG | VG | VG | F | F–P |
| Material cost | $ | $ | $ | $$–$$ | $$$ | $$$ |
Material cost: $ economical → $$$ premium.
Low hysteresis = E means little heat build-up (advantage).
Water rule
Constant humidity, frequent washdowns, hydrolysis
→ POLYETHER (MDI ether or TDI ether)
Oil rule
Oils, greases, diesel, aliphatic solvents
→ POLYESTER (TDI ester or MDI ester)
Dynamic-load rule
Heavily loaded rollers, heavy wheels, high speed
→ NDI first, otherwise PPDI
Thermal & fatigue rule
Continuous service > 90 °C, extreme flexing
→ PPDI
Choosing by need:
economical wear part (no water) → MDI/TDI ester · standard roller or idler → MDI/TDI ether · scrapers, wiper blades, abrasive & oily environments → TDI ester · heavy material-handling wheel / NVH → NDI · high-performance seals and thermal resistance → PPDI · ketones, chlorinated solvents or strong acids → polyurethane is not suitable (consider FKM, PTFE…).Soremag expertise & formulation
Each system is available in many hardness and recipe variants; FDA / food-contact and antistatic / conductive grades on request. All these systems are based on aromatic isocyanates and yellow under UV with no notable loss of mechanical properties. Handling is regulated (diisocyanates — REACH training required). Non-contractual document — indicative values; testing under real conditions recommended. | 🌐 soremag.com · ✉ info@soremag.com · 📞 450-664-4000 | Hot-cast industrial polyurethanes — system selection guide REV. 2025-01 · © 2025 Soremag Inc. |