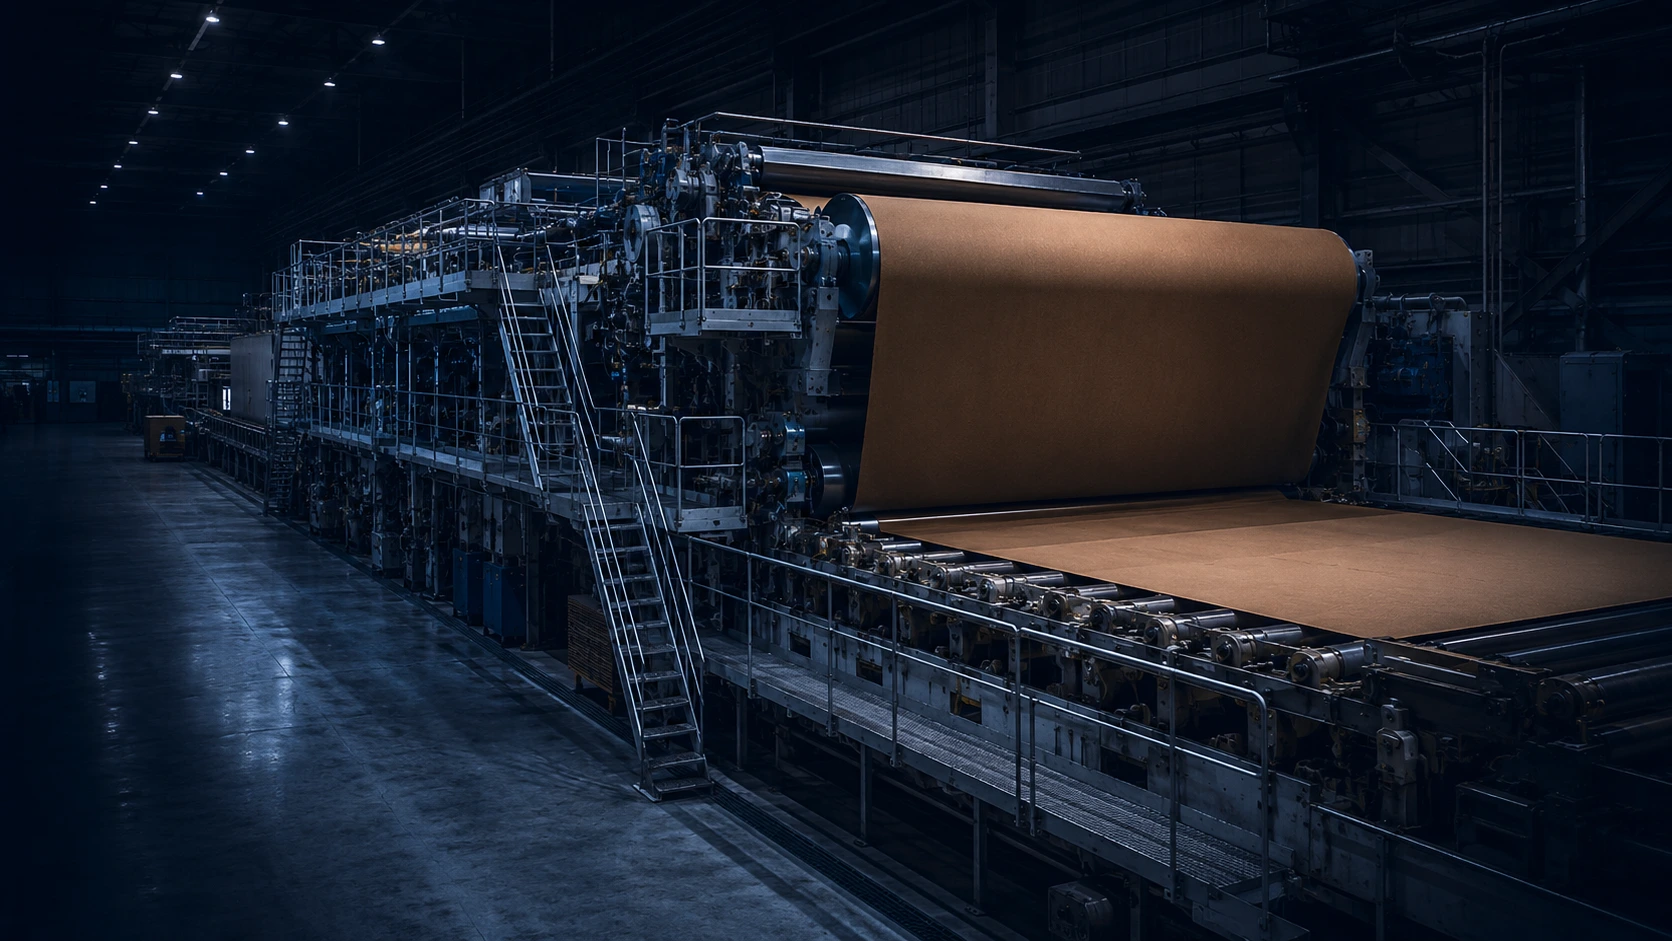
Corrugator, glue unit, flexo printing, rotary die-cutting, folder gluer: a feed roll that slips, a wheel that crushes the flute, a worn anvil cover or starch dust that builds up will run your waste up and your output down in a hurry. We cover and refurbish your rollers, wheels and wear parts — without marking the sheet.
Corrugated is a severe application: paper and starch dust, water-based glues (starch) or hot melt/PVA, abrasion, high speeds and a real risk of marking. It all comes down to the balance: enough friction (grip) to drive the sheet without ever crushing the flute (low-crush).
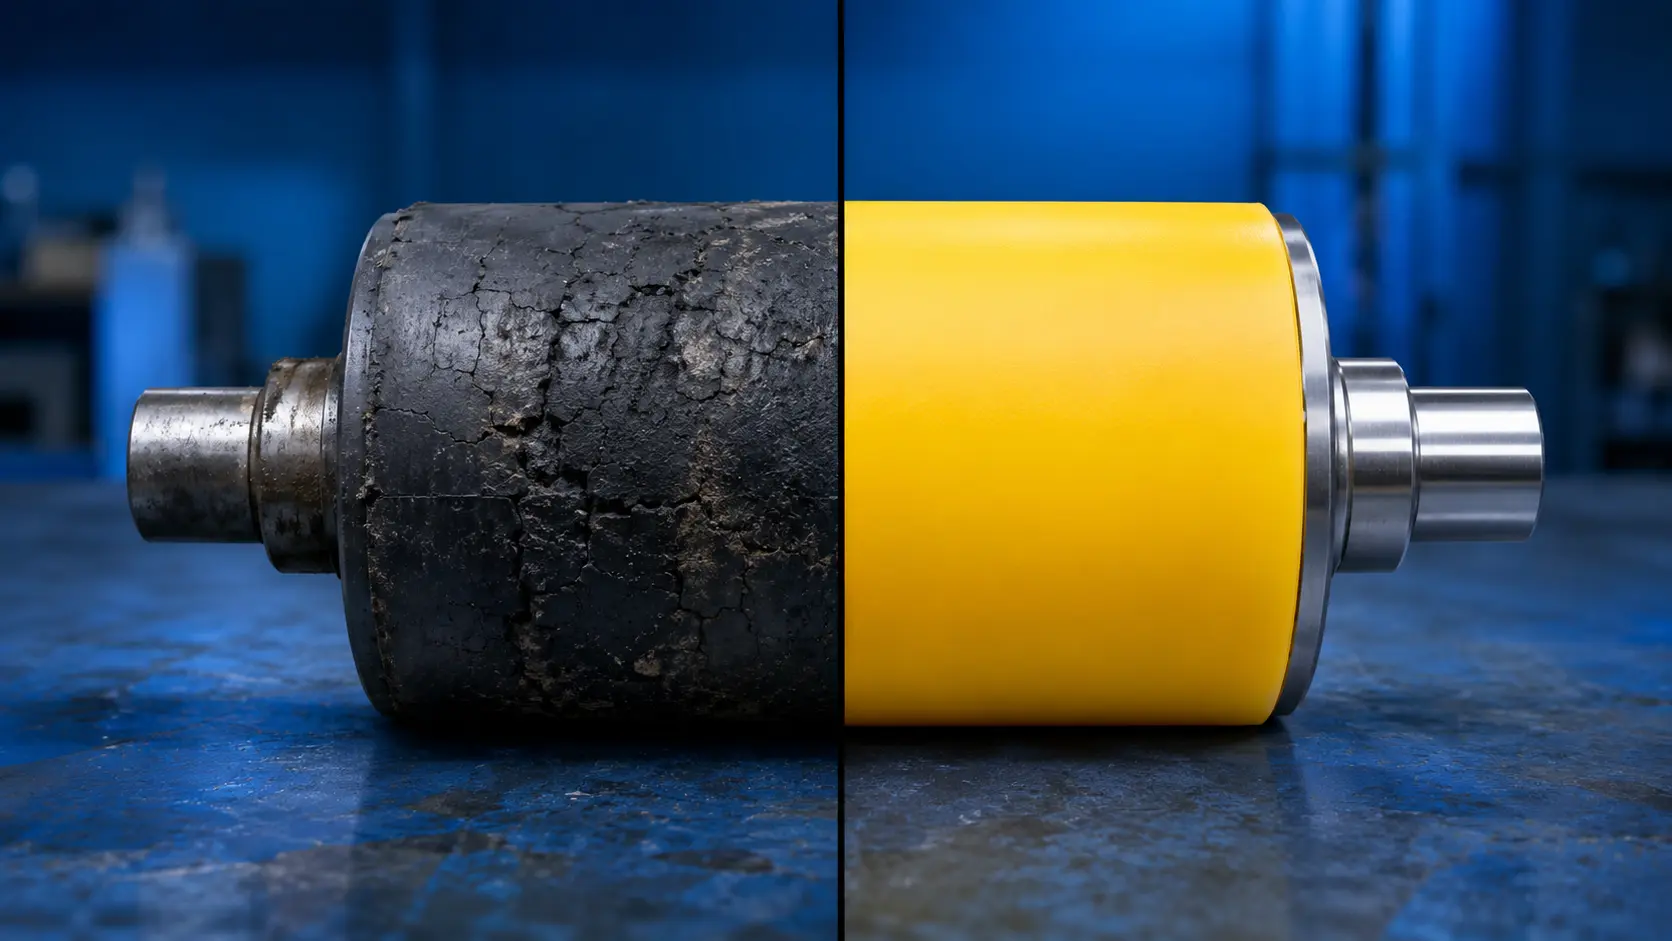
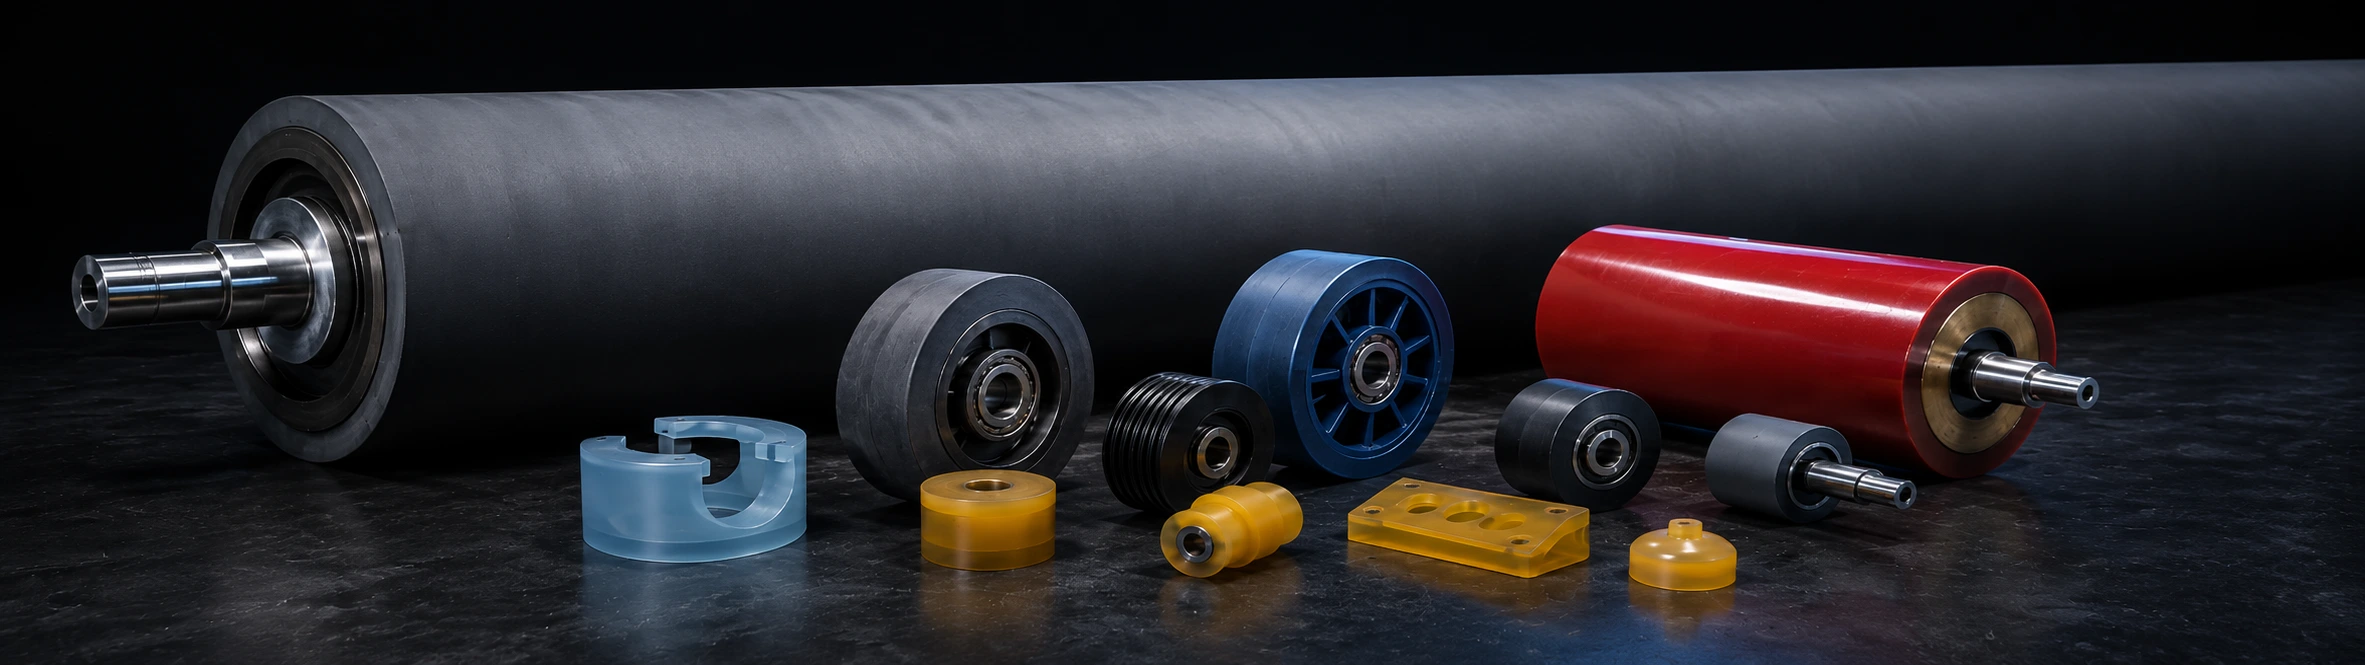
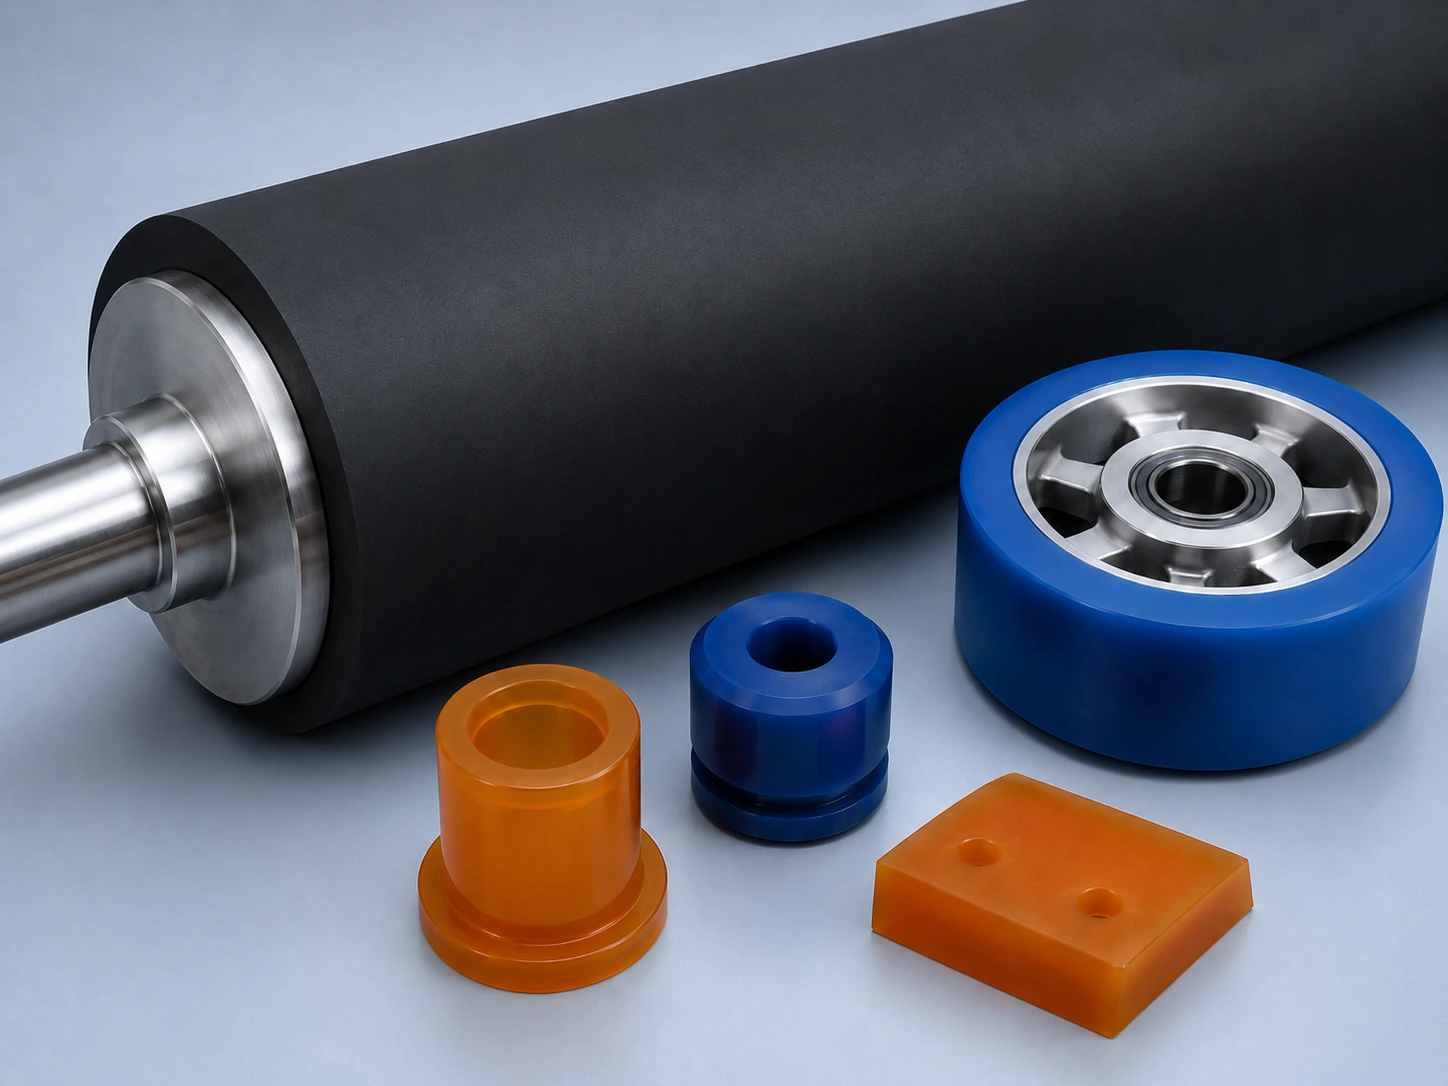
At Soremag, we cover, grind and groove rollers and wheels in rubber or polyurethane, we make cast polyurethane parts (including anvil covers, subject to feasibility) and we repair cores, journals and geometries. The right choice depends on the machine position, the glue, the dust, the speed, the surface finish and the risk of marking.
Feed/pull rolls, nip rollers, transfer, no-crush wheels. The heated corrugating rolls stay steel (outside our scope).
Nip and backing rollers that stand up to starch glue. The engraved applicator roll and the doctor roll stay metal.
Pressure rollers, transfer, infeed/outfeed. The engraved anilox roll stays outside our scope.
Polyurethane anvil covers and wear parts — depending on the model and feasibility.
Feed/pull rolls, transfer, drive wheels and no-crush, polyurethane guides and cleats.
Reverse engineering, geometry adjustment (crown), grooving, journal repair.
Controlled grip and low crush (low-crush) at high line speed.
Uniform pressure; in the glue section, a material compatible with starch.
Sheet transport without marking; surface and concentricity.
In polyurethane for rotary die-cutting — depending on the model, the dimensions, the locking system and feasibility.
Sheet feeding without crushing the flute.
Post-print printing: stable surface, no barring. Anilox excluded.
Fast replacement on the existing shaft, when the assembly allows it.
Guides, cleats, pads, bumpers, wear parts; reverse engineering when the OEM part is unavailable.
Soremag is a

Nip, press and backing rollers: pressure that creases without crushing the flute.
Voir la page
Feed and pull rolls: grip that survives the paper dust that polishes everything.
Voir la page
Transfer and guide: keeping the sheet in line between stations, at full speed.
Voir la page
The sleeve goes to the shop while your shaft stays right where it is on the machine.
Voir la pageStarch or hot melt adhesive, dust and abrasion, speed, finish and marking risk.
The dominant constraint in corrugated is the glue — and it dictates the choice. Aqueous, alkaline and hot at the glue unit; hot and sticky at assembly. The rest of the line is then chosen for dust and ink.
Glue unit, starch adhesive
Excels in hot alkaline solutions and against ozone.
Keep it away from mineral oils, which it will not take.
Hot adhesives and sticky zones
Release and heat resistance.
Vulnerable to cuts and abrasion.
As soon as water is involved
The abrasion resistance of urethane without the hydrolysis risk.
The right call against hot wet starch.
Anvil covers, dry no-crush wheels
Excellent abrasion and cut resistance.
The classic trap: it degrades by hydrolysis in hot wet starch.
Printing and handling
Takes oils, greases and flexo inks well.
Good general abrasion resistance.
Feed rolls and pull rolls
More abrasion resistance and stable grip despite paper dust.
Better ozone and aging resistance than nitrile alone.
Transfer and everyday duty
Economical, good abrasion resistance — press and conveying rollers.
The default when no chemical constraint applies.
Traction
Strong grip, high rebound, low heat build-up.
Avoid where there are oils, ozone or UV.
Starch adhesive is
The answer is
| Symptôme en usine | Ce qu'on ajuste le plus souvent |
|---|---|
| Le carton glisse à l'alimentation | Composé grip + dureté + fini de surface (Ra) + nettoyage de la poussière + rainurage. |
| Le rouleau marque ou écrase la cannelure | Recouvrement low-crush (dureté adaptée) + rectification + contrôle du TIR. |
| Accumulation de colle / d'amidon | Matériau compatible + fini facile à nettoyer + silicone anti-adhérence au besoin. |
| Revêtement d'enclume usé (découpe) | Anvil cover en polyuréthane haute résistance à la coupe — réusinage ou remplacement selon modèle. |
| Usure rapide (poussière abrasive) | Polyuréthane ou caoutchouc haute résistance selon le poste et l'humidité. |
| Vibration / faux-rond / marques cycliques | Rectification, concentricité (TIR), équilibrage, réparation des portées. |
| Revêtement gommant en zone d'encollage | Éviter le PU ester (hydrolyse) → EPDM ou PU éther adaptés à l'amidon. |
A plant is losing box compression strength (ECT): its
What we measure and validate: hardness (Shore A / D), surface finish (Ra), runout (TIR), cylindricity, profile / crown, grooving, dynamic balancing, condition and rebuilding of the journals, adhesion of the cover to the core, chemical compatibility (test on a sample).
To be straight with you: some corrugated components are not covered rollers. The heated corrugating rolls on the corrugator (chrome-plated steel / carbide), theengraved glue applicator roll and the doctor roll, plus the anilox (laser-engraved ceramic) remain specialized metal parts, serviced by their own specialists. Soremag works on everything around them: covered rollers and wheels, anvil covers and polyurethane wear parts. Need help choosing the material? See the material selection guide.
Even if your machines carry another name, describe the function: we will find our way around it.
Brands listed for reference only; Soremag is an independent manufacturer and repairer of rollers and elastomer/polyurethane parts, with no affiliation with these manufacturers.
No. Corrugating rolls are metal (chrome-plated steel or tungsten carbide). We work on the covered rollers and wheels around them: feed/pull rolls, nip rollers, no-crush wheels, transfer and wear parts.
Yes, it is a good application for polyurethane in rotary die-cutting — depending on the model, the dimensions, the locking system, the durometer and feasibility. We also make the related polyurethane wear parts.
Starch glue is water-based, alkaline and hot: a polyester PU degrades in it by hydrolysis (the cover turns tacky). For those zones, we choose EPDM or polyether PU, and silicone for release.
Usually nip pressure that is too high to make up for a lack of grip. We review the compound, the durometer, the finish (Ra), the runout (TIR), cleanliness and sometimes grooving: a low-crush cover brings back traction without crushing the flute.
Polyurethane is excellent for abrasion and cutting; some rubbers (NBR/PVC, NR) give better grip. The choice depends on the position, the glue, the humidity, the speed and the marking risk.
Yes for covered pressure, drive, transfer, infeed and outfeed rollers. Engraved anilox rolls (laser ceramic) and specialized printing cylinders stay outside our scope.
Yes: grooving helps grip, dust evacuation and surface behavior. The pattern is chosen according to what the roller does.
Not necessarily. We can repair, build up and remachine the journals to the original tolerances before covering.
Yes, depending on the part: through reverse engineering, we remake wheels, guides, cleats, pads and cast polyurethane parts.
Talk to a Soremag expert: material, durometer, surface, profile, grooving, anvil cover or mechanical repair. Service in Quebec, Ontario and the Maritimes, with shipping available.
➔ Talk to a technical expert